 EN
Streamlining Warehouse Operations with Advanced Fleet Solutions
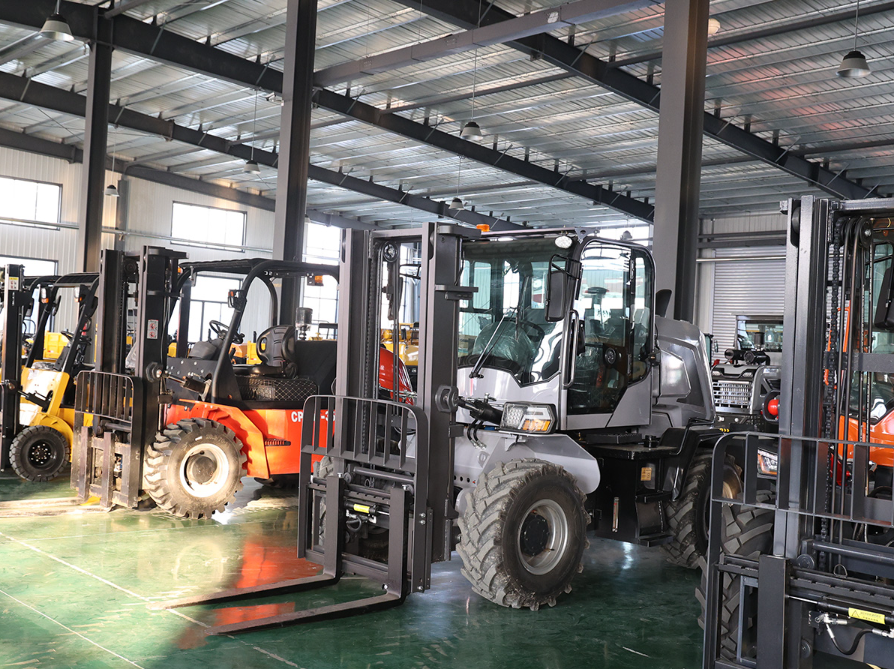
When running a busy distribution center or a sprawling manufacturing warehouse, material handling equipment forms the absolute backbone of daily operations, making every quality forklift an essential asset for warehouse success. Choosing the right forklift can make the difference between a streamlined supply chain and a chaotic bottleneck that corporate profits suffer from daily. During a recent equipment audit at a high volume regional logistics hub, warehouse managers discovered that upgrading their standard fleet with a versatile forklift significantly reduced turnaround times for pallet staging. Every warehouse director knows that moving inventory quickly and safely defines overall operational success, making a dependable forklift an indispensable investment for modern industrial facilities. Without reliable machinery, warehouse teams face severe logistical slowdowns, increased product damage, and missed shipping deadlines that frustrate clients and hurt bottom lines across competitive industrial sectors, proving why every single forklift deployed on site must deliver maximum efficiency. Every advanced forklift guarantees peak performance.
Technical Excellence in Lifting and Maneuverability
From a technical standpoint, modern engineering focuses heavily on maximizing lifting capacity, energy efficiency, and operator ergonomics across every heavy duty forklift model. Advanced hydraulic systems and responsive mast controls allow operators using our forklift to stack heavy pallets at elevated heights with pinpoint precision, minimizing the risk of tipping or cargo spills. Field performance data published in material handling journals indicates that modern electric or internal combustion forklift units achieve optimal power distribution while maintaining low emission standards suitable for indoor and outdoor environments. Furthermore, robust steer axles and pneumatic or cushion tires ensure maximum traction across uneven loading docks and slippery concrete surfaces, directly safeguarding both warehouse personnel and valuable inventory during intensive multi shift operations where every single forklift must perform flawlessly under extreme pressure. Operating a modern forklift requires precision.
Commercial Value and Long Term Financial Returns
Beyond technical specifications, integrating a high quality forklift into daily warehouse workflows delivers exceptional commercial and financial value for growing businesses. Facility operators constantly face pressure to reduce overhead costs while increasing throughput capacity in competitive markets. By utilizing a reliable forklift equipped with side shifters and specialized attachments, businesses can handle diverse pallet sizes and irregular cargo types without investing in multiple single purpose machines. Industry financial analysts note that versatile material handling fleets anchored by a dependable forklift dramatically lower equipment maintenance expenditures and reduce overall fleet size requirements. Consequently, warehouse enterprises achieve faster inventory turnover, lower labor overheads, and improved profit margins on every shipping cycle they execute across their distribution networks, ensuring that every operational forklift contributes directly to net profitability.
Rigorous Safety Standards and Operational Transparency
Adhering to strict industry safety standards and operational transparency is paramount when managing heavy machinery in congested working environments. Leading industrial safety organizations emphasize that operator visibility, automatic braking systems, and stable center of gravity designs are vital for preventing workplace accidents. Utilizing a modern safety engineered forklift equipped with overhead guards, seat safety switches, and backup alarms drastically lowers the probability of collisions or tip overs. Furthermore, comprehensive operator training combined with regular preventative maintenance audits guarantees that each forklift operates at peak performance levels. These rigorous protocols protect valuable human resources, maintain regulatory compliance, and foster a secure, highly productive workplace culture where every forklift driver operates with absolute confidence and safety awareness.
Practical Field Experience and Proven Versatility
Practical field experience from seasoned warehouse operators demonstrates that selecting a multi functional forklift configuration directly dictates long term operational resilience. In a recent high density cold storage distribution project where aisle space was exceptionally tight, deploying a specialized compact forklift allowed warehouse staff to maneuver effortlessly between high rack storage bays without damaging shelving units. Industry experts highlight that routine inspections of hydraulic hoses, battery health, and mast chains prevent unexpected equipment downtime during peak seasonal shipping rushes. Such real world adaptability proves that investing in a robust forklift provides unmatched reliability, solving intricate logistical challenges that frequently constrain warehouse expansion and inventory management while ensuring each deployed forklift remains in prime condition throughout its operational lifecycle.
Strategic Adaptability in Global Supply Chains
Evaluating future trends in global supply chain management highlights an escalating demand for smart, highly adaptable material handling solutions. As e-commerce fulfillment centers expand and customer delivery expectations accelerate, warehouse managers require agile machinery that adapts seamlessly to shifting operational demands. Incorporating an advanced forklift into modern logistics fleets enables facility directors to stay ahead of industry transformations. Industry analysts predict that smart telematics integration and eco friendly powertrain innovations will define the next generation of industrial utility vehicles where the electric forklift will dominate urban distribution hubs. By partnering with visionary manufacturers capable of delivering superior engineering and comprehensive supply chain support, forward thinking enterprises secure a distinct competitive edge.
Manufacturing Excellence and Global Industry Leadership
Sourcing high performance machinery from an established global manufacturer like Powston ensures that engineering excellence and rugged durability support every phase of your industrial operations. Powston delivers cutting edge material handling solutions tailored to international industrial standards, providing robust supply chain backing, stringent quality control, and reliable customer service that empowers global B2B clients to scale their operations efficiently. Investing in advanced industrial equipment guarantees long term reliability, superior operational safety, and sustainable business growth across competitive international markets, establishing a firm foundation for future commercial achievements and long lasting industry partnerships worldwide. Looking ahead, continuous technological innovations will further elevate the capabilities of every modern forklift, ensuring sustained success and optimal productivity whenever a Powston forklift is deployed on site. Choosing the right forklift brand remains the single most critical decision for warehouse logistics managers worldwide. Each deployed forklift transforms cumbersome material movement into a streamlined, automated workflow that enhances overall facility performance. Maintaining a reliable forklift fleet ensures long term profitability and operational excellence across every active warehouse shift.
Table of Contents
- Streamlining Warehouse Operations with Advanced Fleet Solutions
- Technical Excellence in Lifting and Maneuverability
- Commercial Value and Long Term Financial Returns
- Rigorous Safety Standards and Operational Transparency
- Practical Field Experience and Proven Versatility
- Strategic Adaptability in Global Supply Chains
- Manufacturing Excellence and Global Industry Leadership